advanced filtration and dust control for the
Metal recycling industry
Location: Belgium
Industry sector: Metal recycling
This project was carried out by our customer Bofar.
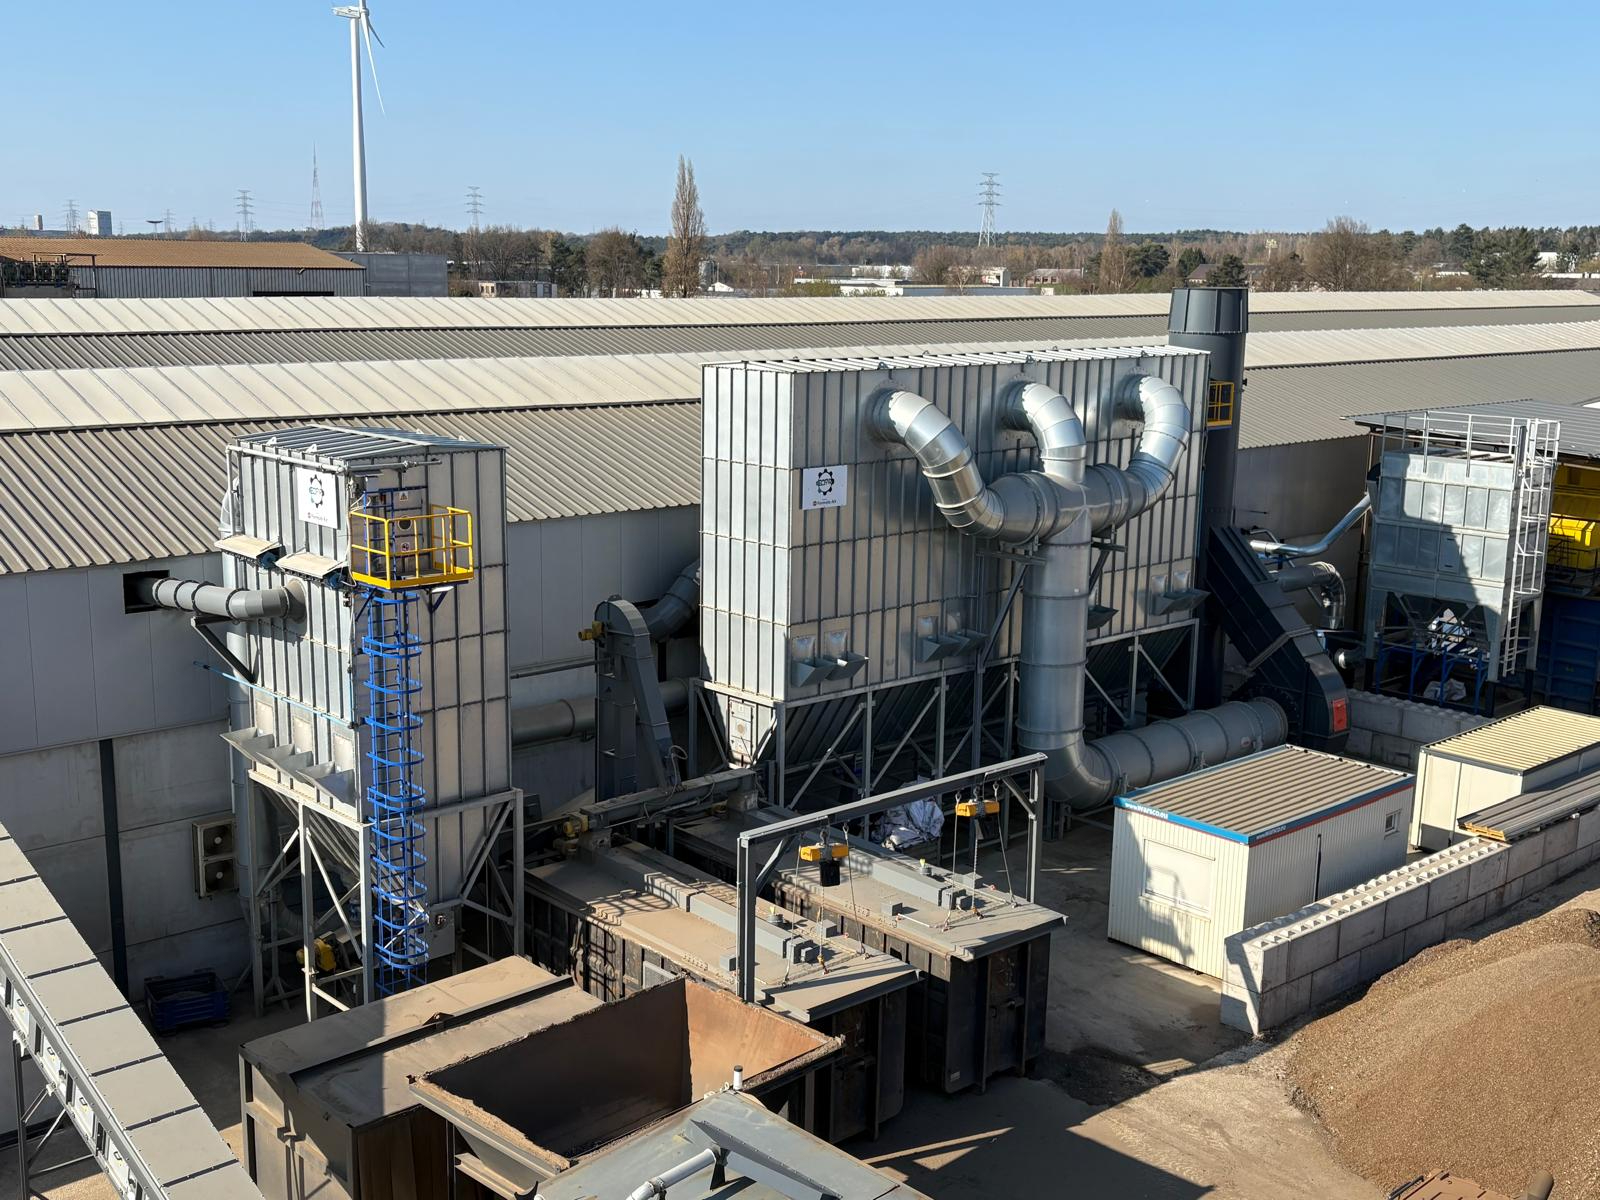
Formula Air supplied Bofar with a total of two complete dust extraction and filtration systems, that were installed at Euregio Recycling production facilities. Through these projects, Formula Air makes an important contribution to creating a safe, sustainable, and efficient recycling environment, minimizing emissions while safeguarding the continuity of the production process.
Background
Bofar, based in Nederweert, specializes in the design, manufacturing, and delivery of tailor-made solutions for the recycling industry. The company primarily focuses on the engineering, production, and integration of complete recycling and separation installations for a wide range of material streams. Thanks to its extensive practical experience, Bofar develops both individual machine components and complete process lines, fully tailored to the specific requirements of its customers. For this project, Bofar worked closely with its customer, Euregio Recycling, to realize an efficient and future-proof dust extraction system.
Euregio Recycling specializes in the processing and recycling of ferrous and non-ferrous metals. Every day, large volumes of mixed scrap metal from various industrial sectors are delivered to the facility. To reintroduce these materials as high-quality secondary raw materials, the scrap undergoes an extensive mechanical processing procedure.The heart of the installation is a powerful shredding plant, where the incoming scrap is reduced into smaller fractions. After the shredding process, the material is transported via a network of conveyor belts to various sorting installations. Within these installations, the different material streams are separated, enabling valuable ferrous and non-ferrous metals to be efficiently recovered for reuse.
Challenge
During both the shredding process and the subsequent sorting stages, significant quantities of fine dust, metal particles, and other airborne particulates are generated. High dust concentrations can especially occur at the shredder, transfer points, and material discharge locations. Effective dust extraction is therefore essential to create a safe working environment, ensure process continuity, and comply with applicable environmental regulations.
Euregio Recycling places great importance on the working and living environment of both its employees and the surrounding area of the production facility. The company continuously invests in sustainable technologies to further reduce emissions and remain prepared for increasingly stringent environmental legislation.
By striving for minimal emissions and maximum process control, Euregio Recycling is taking important steps towards a future-proof and sustainable recycling industry, fully aligned with the ambitions of the European Green Deal.
Solution
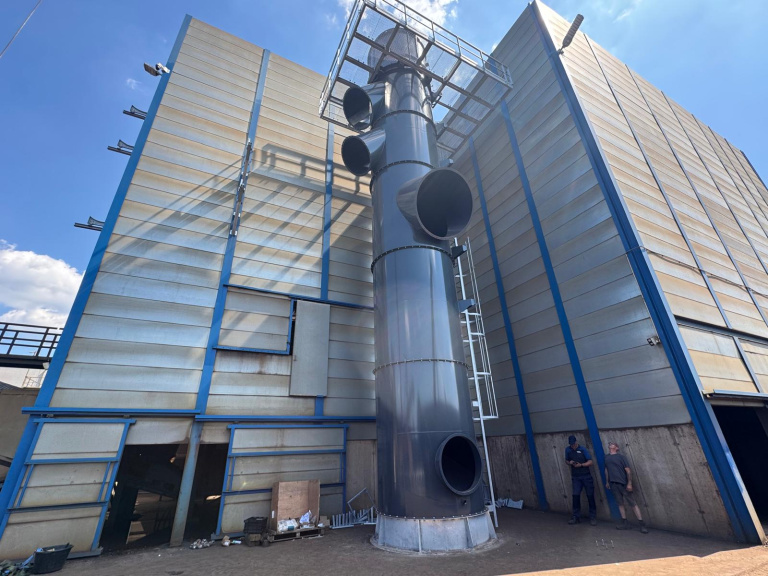
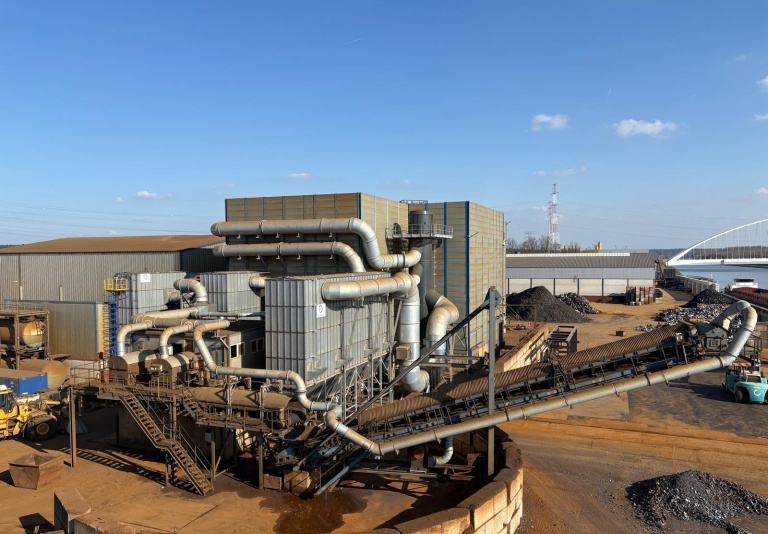
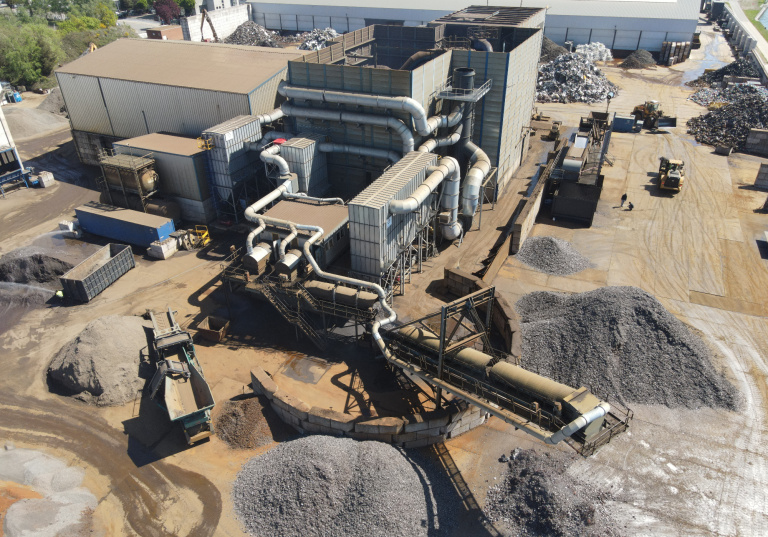
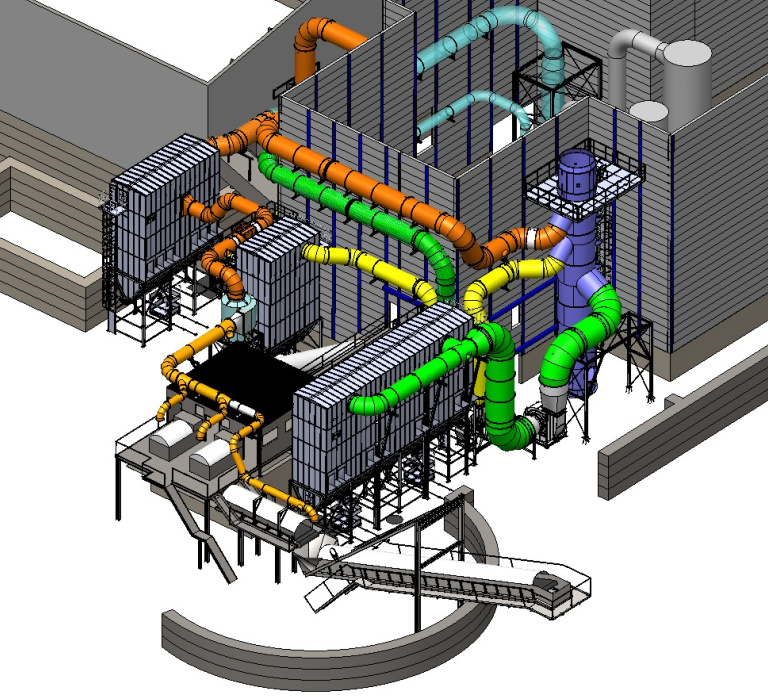
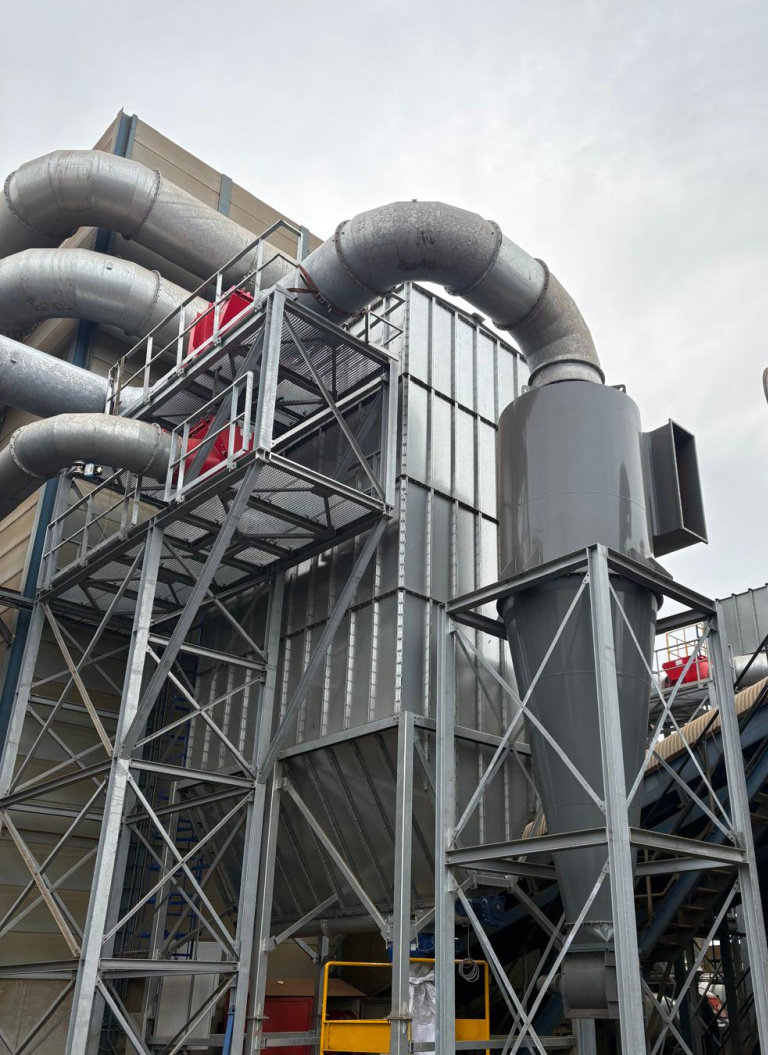
- The first system represents a solution for the extraction and filtration of fine dust generated during both the shredding process and the subsequent sorting processes. This installation has a total extraction capacity of approximately 200,000 m³/h and was entirely designed, engineered, manufactured, supplied, and commissioned by Formula Air. The installation is equipped with extensive explosion protection measures and intelligent control systems to ensure safe, reliable, and continuous operation. The complete solution consists of a combination of standard and specially developed components. Standard components include cyclone filters, bag filters, fans and BADA non return valves.
- For the ductwork, a robust design was selected using thick-walled carbon steel ducting, fully hot-dip galvanized, ensuring a long service life and optimum corrosion protection under the demanding operating conditions within the recycling industry. In addition, various customer-specific components were developed, including ductwork with diameters exceeding standard sizes, support structures, explosion relief devices, control systems, and a Heavy Duty Diverter valve with spark detection system specially designed for this application.
- In addition to this central installation, Formula Air also supplied a second filtration system for a new sorting process. This installation has a total capacity of 140,000 m³/h and consists of an ATEX-certified filtration unit with a capacity of 20,000 m³/h and a high-capacity filtration system with a capacity of 120,000 m³/h. Formula Air was also responsible for the complete engineering, manufacturing, and integration of this installation within the existing process environment.
Dust Extraction System Components
The installation was designed as a fully integrated system, combining dust extraction, filtration, air transport, and safety technologies to ensure reliable and efficient operation, comprising the following key components:
Cyclone Separator FA 1
Bag Filter Systems:
● 110,000 m³/h
● 50,000 m³/h
● 35,000 m³/h
● 120,000 m³/h
● 20,000 m³/h (ATEX)
Fans:
● 250 kW
● 132 kW
● 90 kW
● 250 kW
● 37 kW
Chimney Ø2300 mm, height 16,500 mm
Chimney Ø1900 mm, height 12,500 mm
Spark detection system and a custom-built Heavy Duty Diverter valve
BADA non-return valves
Ductwork
Overpressure relief valves
Why Formula Air
Formula Air was selected as a trusted partner thanks to its ability to provide a complete turnkey solution, combining all required technologies within a single project scope. The customer particularly valued Formula Air's engineering expertise, practical approach, and proactive involvement throughout the project. This added significant value during the design and implementation phases, including the successful development of a custom-engineered Heavy Duty Diverter Valve and spark detection system capable of withstanding the extreme conditions associated with potential shredder explosions. By actively identifying opportunities for optimization and process improvements, Formula Air helped deliver a safer, more efficient, and future-proof solution.
Impact and results
Thanks to the implemented dust extraction and filtration systems, Euregio Recycling now operates a future-proof installation that complies with current European emission legislation and is prepared for future tightening of environmental requirements. Through the application of advanced filtration technologies, emissions of dust and other harmful components are reduced to a minimum.
In particular, emissions of PCBs and dioxins substances that require special attention within the metal recycling industry due to their impact on both human health and the environment have been significantly reduced. As a result, the installation not only ensures compliance with current legislation and regulations, but also supports Euregio Recycling's ambition to further reduce the environmental impact of its operations and maintain a sustainable and responsible business approach.
Beyond reducing emissions, the installation helps safeguard Euregio Recycling's core business operations. By ensuring compliance with current and future environmental requirements while reducing operational costs, the solution provides a strong return on investment and supports the long-term continuity of the recycling facility.